Recovery of slop oil,
oily sludge, bilge water
and industrial process water
We treat oily waste right where it is produced: three-phase separation on site
that recovers the oil and cuts volumes, transport and disposal costs
Slop oil treatment, plug & play,
fully equipped
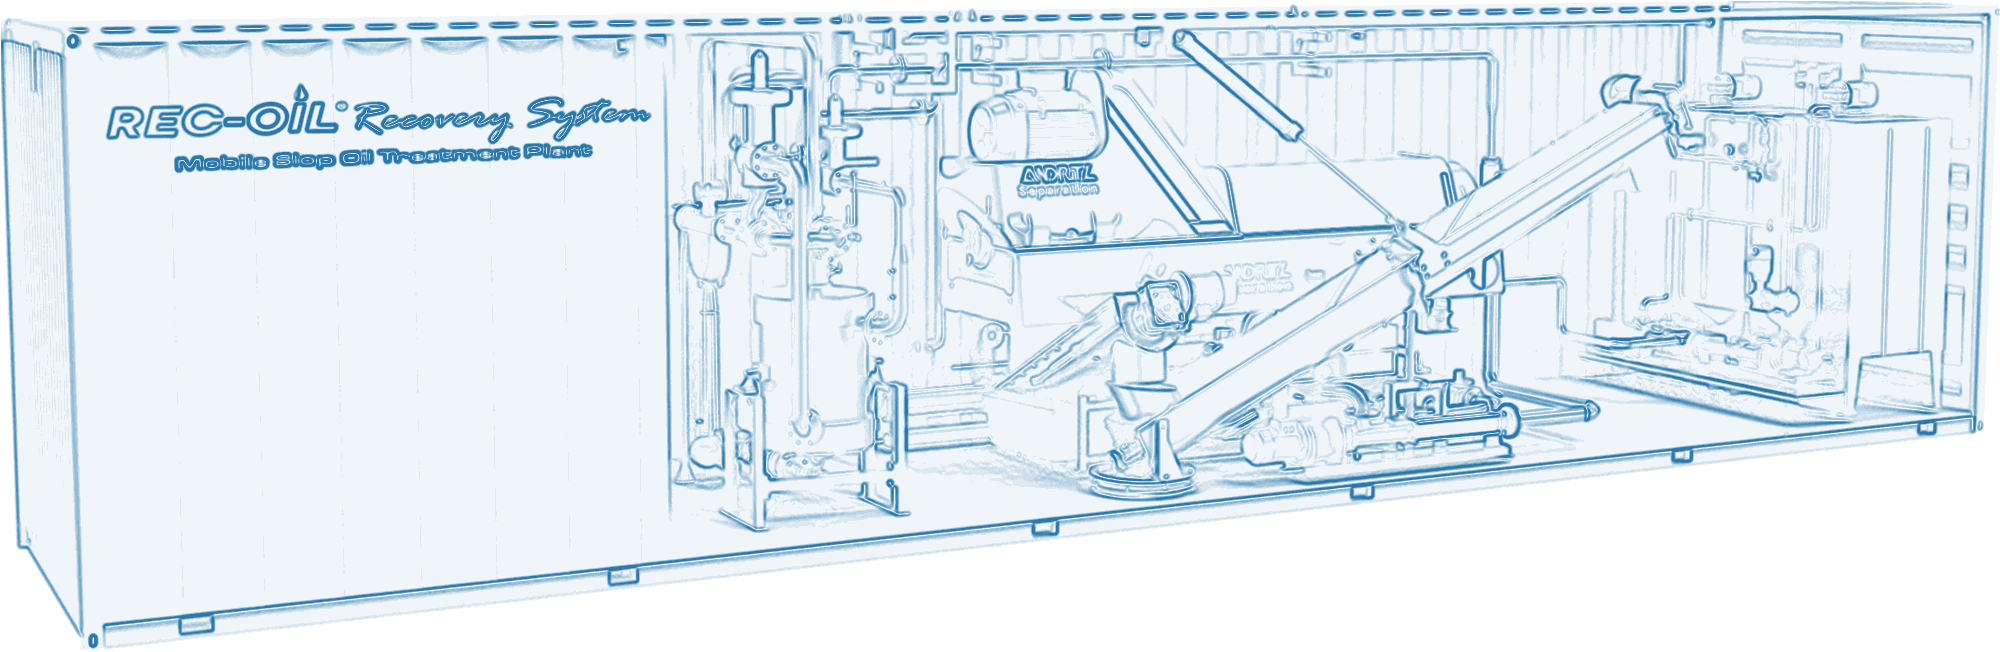
Suction, separation, recovery and control in a single containerised system, with all ancillary equipment included. It arrives on site, connects and gets to work. No assembly, no suppliers to coordinate
The REC-OIL plant for slop oil and oily sludge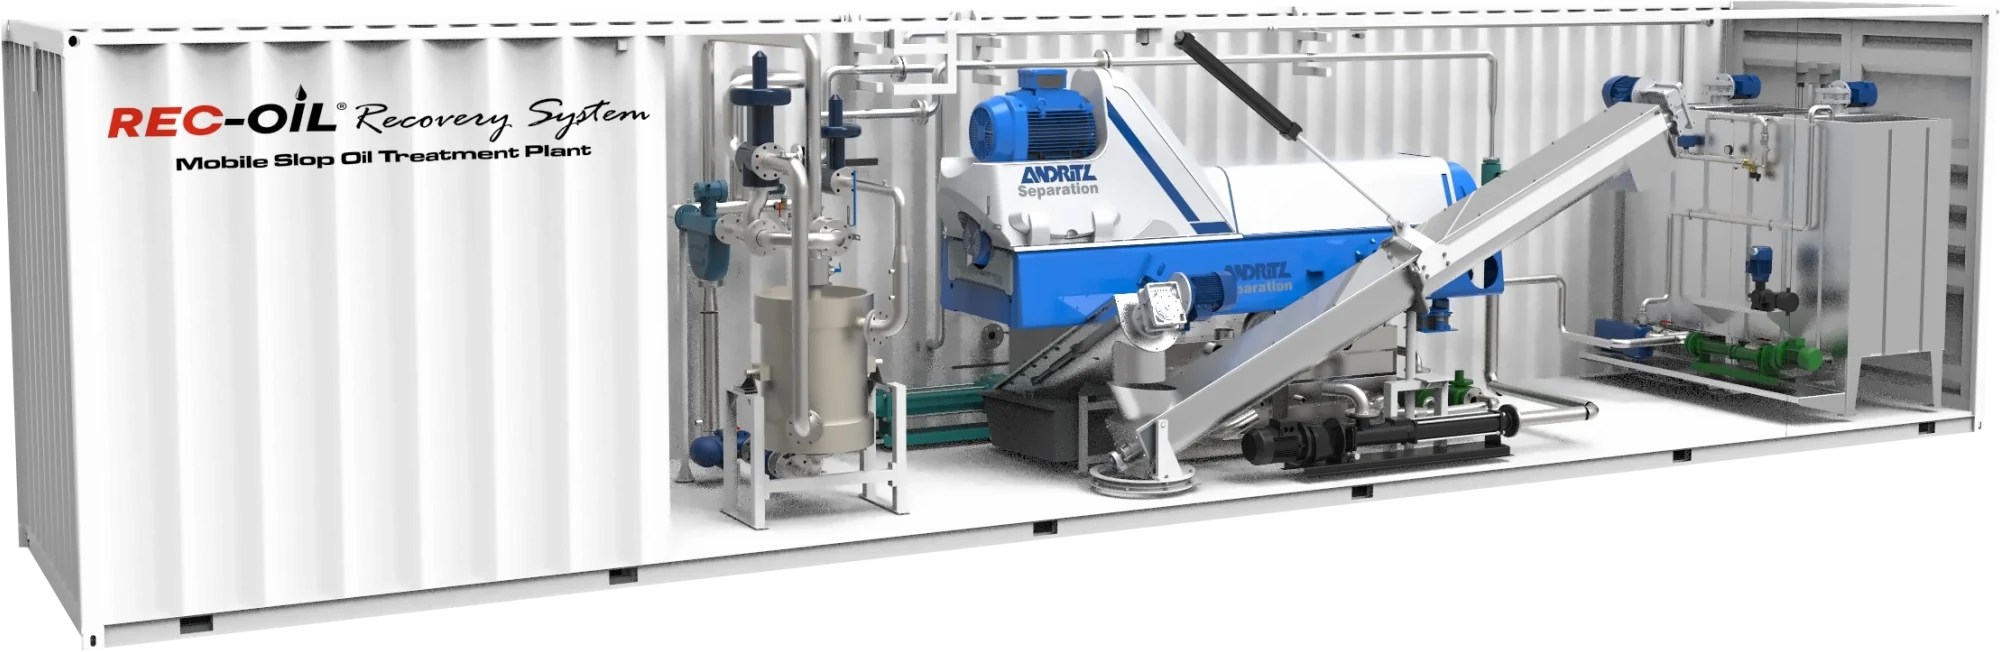
The slop changes,
production has to stop
Oil, water and solids arrive in ever-changing proportions.
With a fixed plate dam, every change in the feed means shutting down, waiting for the bowl to cool, undoing twelve bolts and starting again
The feed changes,
the plant keeps producing
Andritz’s patented “pipette” system adjusts continuously:
no shutdown, no cooling, no plate dam to replace; the machine follows the slop and production never stops
It adjusts while running,
oil exits under pressure
Water leaves by gravity; the pipette collects the oil and discharges it under pressure.
It moves in millimetre steps with the machine running and sets the oil level in the bowl, without undoing a single bolt
Slop oil in,
water, oil and solids out
- 01SuctionSludge pumpSlop enters the containerAmbient temperature
- 02HeatingSpiral heat exchangerSteam brings the mixture up to temperatureFrom ambient to 85-95 °C
- 03MeasurementMass flow meterContinuously measures the incoming flow rate85-95 °C
- 04ConditioningPolyelectrolyte and demulsifierDosed in line to prepare for separation85-95 °C
- 05SeparationAndritz 3Ph ATEX decanterWater, oil and solids separated continuously85-95 °C
less than 1% solids
less than 1% solids
A single electrical panel runs the whole process
ATEX certified,
it works at the source
Designed to operate inside the hazardous area, with no transfers out of the zone and no exemptions to request
Same plant, 23% more productivity
Each square is one month, one row per year
Payback comes in half the time because the pipette decanter runs 4,000 hours a year instead of 3,250 and recovers 98% of the oil instead of 85-92%. That is 7,500 m3 more slop treated every year
Sample calculation: REC-OIL plant for cleaning slop oil tanks, flow rate 10 m3/h, two shifts and two feed changes per day. Comparison between an Andritz decanter with pipette system and a standard decanter with fixed plate dam, with the rest of the plant unchanged
Oil & gas applicationsBacked by
an industrial group since 1988
IFA Industry is part of Tecnoaria Group: five coordinated companies that design, install and service industrial plants, each specialised in one part of the supply chain
Your project,
let’s talk about it
Request sent
Thank you, an IFA engineer will get back to you to discuss your case